Laser Cutting
& Sheet Metal
Cut, formed, welded and finished sheet metal — enclosures, panels and cabinets, where the part is usually fine and the assembly is where it goes wrong.
Processes we buy
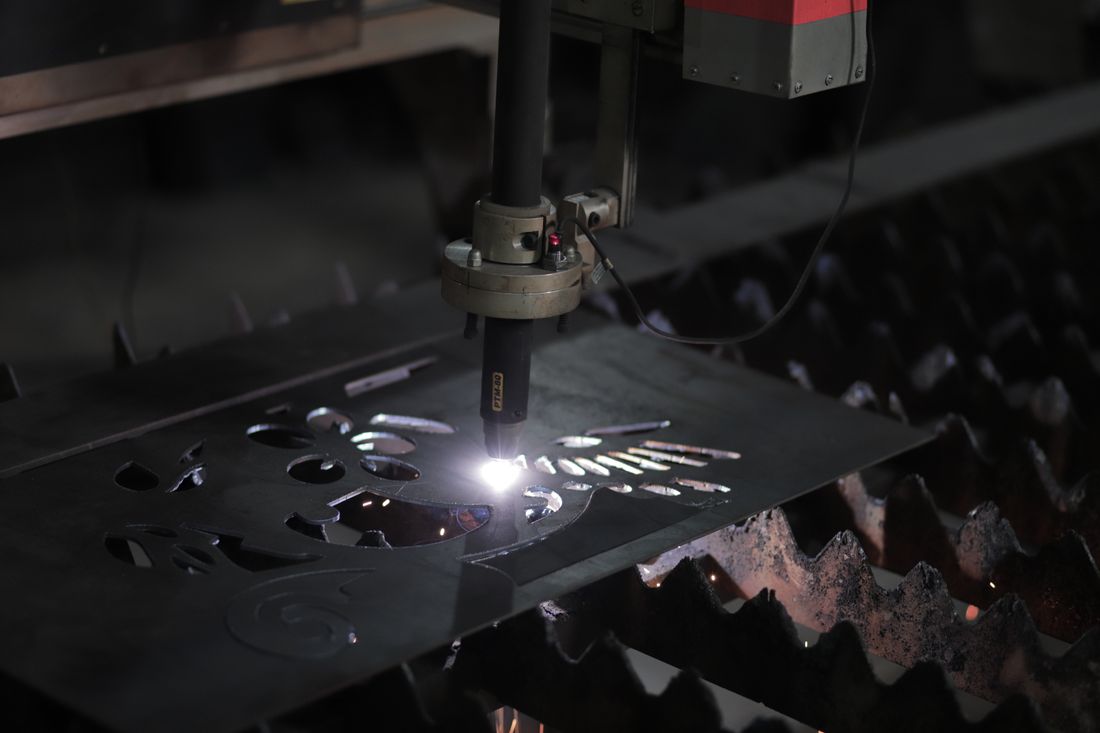
- Laser cuttingFibre and CO₂ on mild steel, stainless and aluminium.
- Turret punchingWhere the part is hole-dense and the volume suits a turret.
- Press brake formingCNC bending with tooling and bend sequence specified.
- Welded assembliesMIG, TIG and spot, with weld symbols and inspection agreed.
- Enclosures and panelsCabinets, chassis, panels and racks with hardware fitted.
- FinishingPowder coat, plating, passivation, silk-screen and assembly.
What we fix before cutting
These goods are bought to a drawing, a grade and a tolerance. That only works if the drawing is controlled, the features that actually matter are named, and the supplier can measure them repeatably.
Every criterion above appears in the inspection report as a pass or a fail, with the measured value beside it and the gauge named. A first article is signed off before any bulk is produced.
What we screen before a sample is quoted
Tolerance stack-up
Every bend is within tolerance and the finished cabinet still does not close. Assembly-level tolerance is agreed up front, because it is the one that matters.
Weld quality
Cosmetically ground welds hiding poor penetration. Where it is structural, inspection method and acceptance are named before production.
Coating adhesion
Inadequate pre-treatment shows up as field failures months after arrival. Adhesion and salt-spray expectations are set on the sample.
Fume and safety
Laser fume extraction and welding ventilation are routine audit findings in smaller fabrication units.
Clusters we work for this line
Sheet metal is the easiest capability to acquire and the hardest to do consistently. The gap between units inside one industrial estate is very wide.
The other manufacturing lines
Send us the sample. We will tell you honestly.
Whether we can source it well in India, what it should cost, and what could go wrong — before you commit to anything.